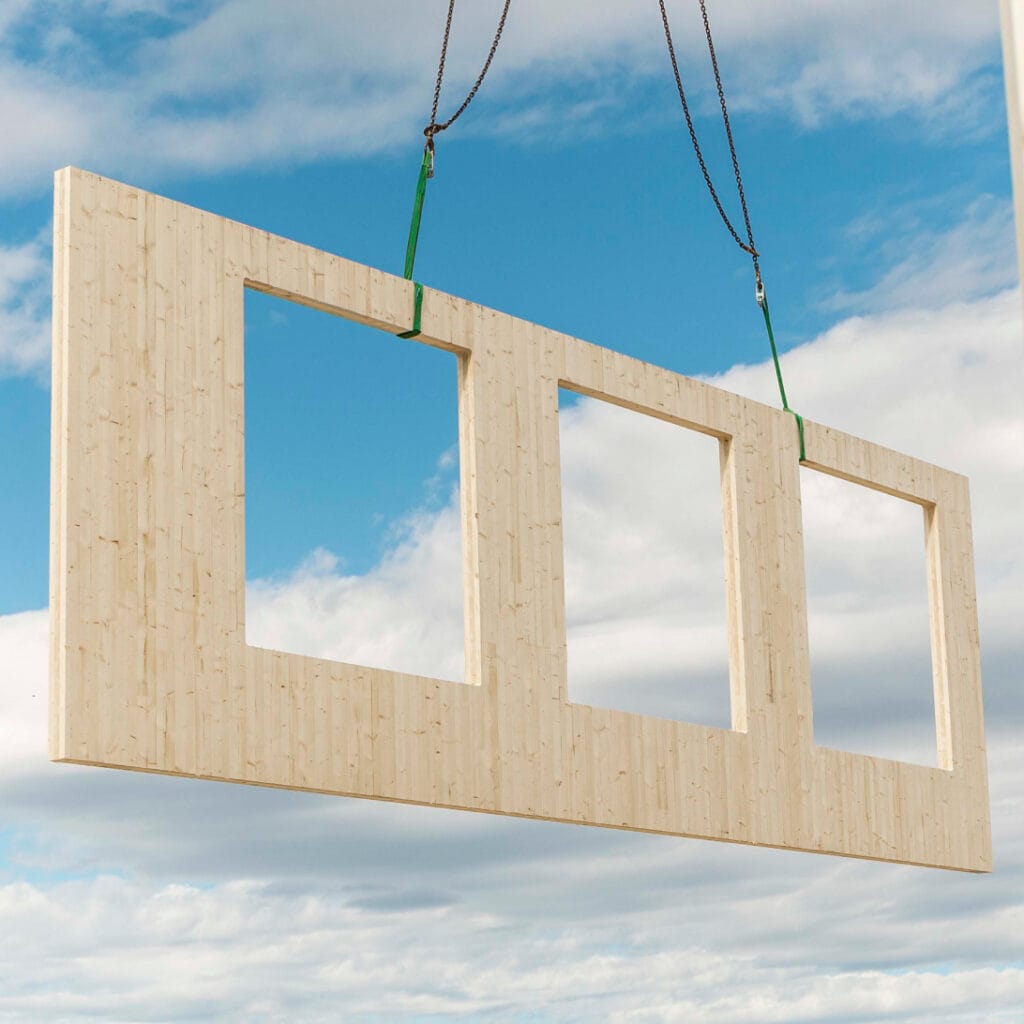
Building with Cross-Laminated Timber – From Felling to Completed Building
Splitkon AS has 78 employees who collectively have extensive experience from the Norwegian timber industry. Splitkon’s engineers undertake all necessary design and engineering documentation required to ensure that manufacturing, processing and assembly proceed as planned.
Felling
Cross-laminated timber from Splitkon is manufactured from Norwegian spruce. Norwegian forests are well managed, and all timber we use is PEFC-certified – which means there is assurance that the forest is managed in accordance with laws and regulations and takes into account renewable operations and protected nature. By using Norwegian timber, we also support one of Norway’s primary industries
The Factory
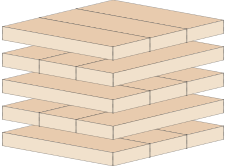
Our fully automated factory is fed with Norwegian timber at one end, and through the modern production line the lamellae are sorted, cut, planed, glued and pressed together to form cross-laminated master panels. The panels then pass through large processing machines that cut the elements to the customer’s specification. Finished elements are packaged and placed on pallets awaiting transport.
Logistics
The finished processed elements are loaded in the correct sequence onto semi-trailers, so that when they arrive on site they can be lifted straight into position in the structure and installed where they belong. This means that building with cross-laminated timber happens extremely quickly and that the on-site process is efficient and accurate.
Completed Building
The possibilities of using cross-laminated timber from Splitkon are endless. Timber is malleable, and its load-bearing capacity in relation to its weight is unparalleled. Cross-laminated timber is the only renewable building material we have. As if these weren’t good enough reasons to choose cross-laminated timber from us, we remind you that timber products sequester CO2 throughout their entire lifespan, and with proper maintenance we’re talking about up to 100 years!
The Process
Already during the tender process, calculations have been made regarding which raw materials and quantities are needed to deliver optimally in a project. Splitkon procures timber quarterly and sources PEFC-certified timber from nearby sawmills. This ensures that we use Norwegian spruce of very high quality in our CLT manufacturing.
From experience, we know which dimensions we need most. However, it is only when the IFC model of the building has been detailed by the structural engineer, engineer and architect, and subsequently finalised by Splitkon’s structural engineer, that we know which raw materials we need and the project proceeds to the manufacturing department.
Here we nest for optimal production and create a delivery plan. This is designed to provide the most efficient production possible, minimal intermediate storage at the factory, and ensure that the elements are delivered to the construction site as close as possible to the assembly sequence.
Master panels are divided into elements and receive the correct cut-outs using CNC machines. Elements are the final product to be delivered to the construction site.
Throughout a project, manufacturing maintains ongoing dialogue with the project manager and structural engineer for the best possible monitoring of the construction site. Deliveries to a project are always quality assured before leaving the factory.